Manufacturing Process
Seven Stages.
One Consistent Yarn.
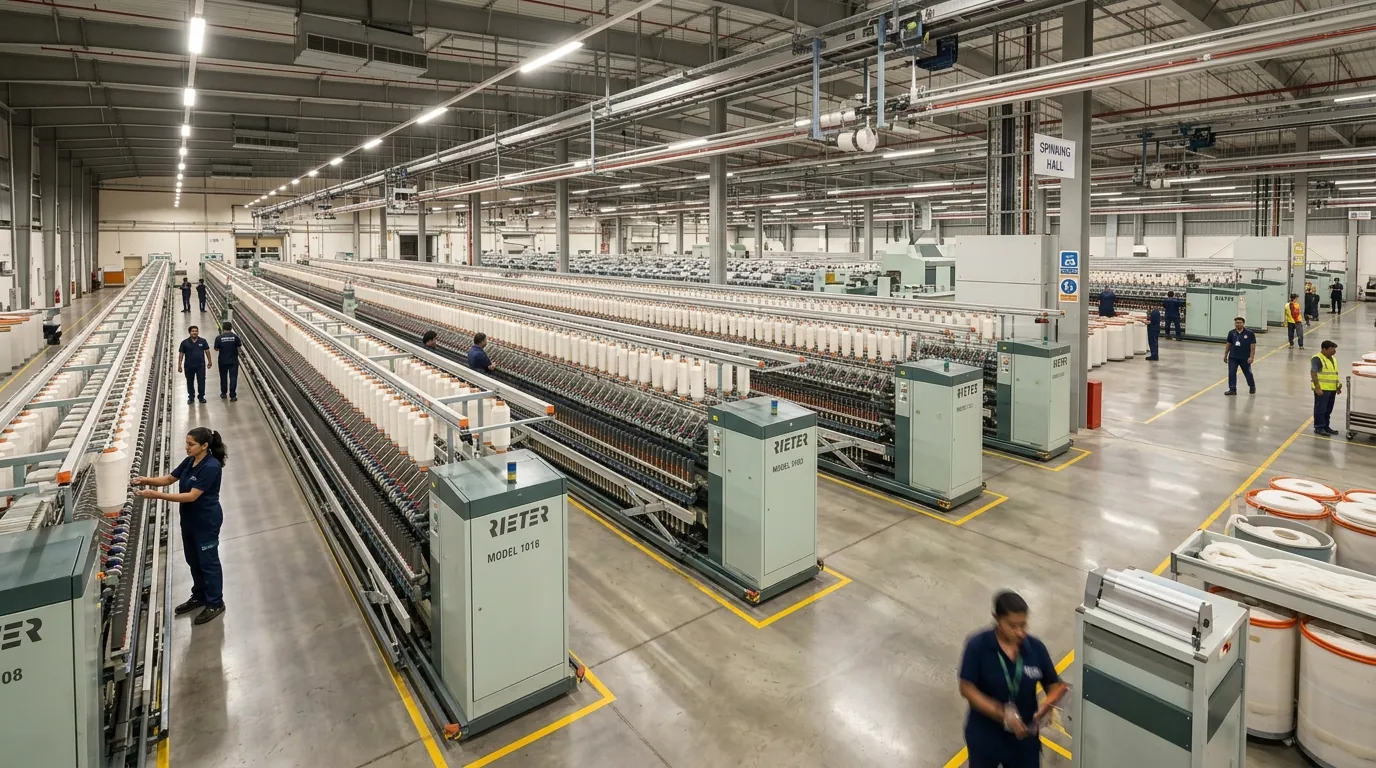
Every cone of AKR karded yarn passes through a structured, seven-stage ring spinning process. Understanding how we make it helps you understand why you can rely on it.
Opening & Cleaning
LMW & Trützschler Full LineRemove impurities and open raw cotton and blend fibres
Raw cotton bales and synthetic fibres are opened on our automated Trützschler and LMW blowroom lines. A synchronized sequence of coarse and fine openers, dust extractors, and micro-cleaners separates the fibres gently while removing leaf particles, seed coats, and micro-dust without fibre degradation.
Trash content and fibre tuft regularity monitored continuously at blowroom exit.
Carding
Trützschler & LMW High-Production CardsIndividualize fibres and extract remaining neps and short fibres
Treated fibres pass through high-production Trützschler and LMW carding frames. Precision revolving wire flats individualize tangled clumps into singular parallel fibres, systematically removing neps and short fly waste to deliver a clean, uniform sliver.
Sliver weight (hank), nep count, and short fibre percentage tested at card delivery.
Drawing & Doubling
LMW & Rieter Autoleveller Draw FramesImprove sliver evenness, parallelize fibres, and blend components
Multiple card slivers are combined and drafted on Rieter and LMW autoleveller draw frames. Digital autolevelling compensates for sliver mass variations instantaneously, ensuring perfect fibre parallelism and uniform blend distribution for 100% cotton, PC, and CP yarns.
Sliver evenness (CV% < 0.6%) and linear density verified with continuous autoleveller monitoring.
Roving / Simplex
LMW Speed FramesAttenuate sliver and apply protective twist for ring spinning
The drawn sliver is drafted down on LMW speed frames and given a controlled protective twist to create a slender roving. Roving bobbins are loaded onto overhead creel tracks to eliminate manual handling shocks before ring drafting.
Roving count (hank), twist factor, and bobbin tension uniformity verified.
Ring Spinning
LMW Ring Spinning FleetDraft, insert final twist, and spin into finished yarn
Precision LMW ring frames draft the roving to the exact yarn count (Ne 16s to Ne 60s) and insert the final twist through synchronized ring-and-traveller mechanisms. Spindle speeds and drafting zones are tailored for each count to ensure optimal tensile tenacity and low hairiness.
Count (Ne), twist-per-inch (TPI), breaking tenacity (cN/tex), and elongation tested regularly on spindle doffs.
Autoconer Winding
Saurer & Muratec Precision AutoconersTransfer to export cones, clear defects, and thermo-splice
Yarn is wound from spinning bobbins onto delivery cones on Saurer and Muratec automatic winding machines. High-speed electronic yarn clearers scan every centimetre, cutting out thick spots, thin places, and neps, replacing them with knot-free splices.
Electronic clearer settings verified; splice strength tested; cone density checked for high-speed knitting and warping.
Testing & Quality Release
Uster Benchmarked Testing LaboratoryVerify lot-to-lot parameters meet global standards before dispatch
Yarn packages from each production lot are conditioned and tested in our laboratory against Uster global benchmark standards. Measurements cover count variation (CV%), tensile strength, elongation, mass evenness, imperfection indices, and hairiness before release.
Full Uster testing, tenacity testing, and comprehensive lot test certificates generated for buyer inspection.
For Buyers
What This Process Means for Your Order
Consistent Count
Count variation (CV%) is controlled at drawing, roving, and monitored at ring frame and testing. Consistent count means consistent fabric weight.
Controlled Imperfections
Yarn clearers at winding remove thick places, thin places, and neps from the delivery package. Imperfection levels are tracked against Uster benchmarks.
Reliable Strength
Tenacity and elongation tested on finished yarn ensure each lot has the mechanical performance required for your knitting or weaving application.
Lot-Level Quality Data
Each production lot is tracked through the process. Quality data is available for discussion when you place an enquiry for a specific specification.
Let's Work Together
Partner With AKR Spinning Mills
Experience the difference of precision-engineered yarns backed by decades of expertise. Contact our team to discuss your specific textile requirements.